

China’s manufacturing sector is undergoing a significant transformation as industries place greater emphasis on precision, safety, and product reliability. From electronics and automotive components to food processing and pharmaceuticals, businesses are increasingly adopting advanced inspection technologies to meet evolving production standards. Among these technologies, X-ray inspection systems have emerged as an essential tool for identifying hidden defects and maintaining consistent quality control.
The growing integration of automation and smart manufacturing practices is also expanding the role of digital inspection solutions. Modern X-ray systems are capable of performing non-destructive testing, allowing manufacturers to examine the internal structure of products without causing damage. According to the China X-Ray Inspection System industry analysis by Markntel Advisor, the technology is gaining wider relevance across multiple industrial applications as companies seek higher operational efficiency and improved compliance with quality standards.
Why X-Ray Inspection Systems Have Become Essential
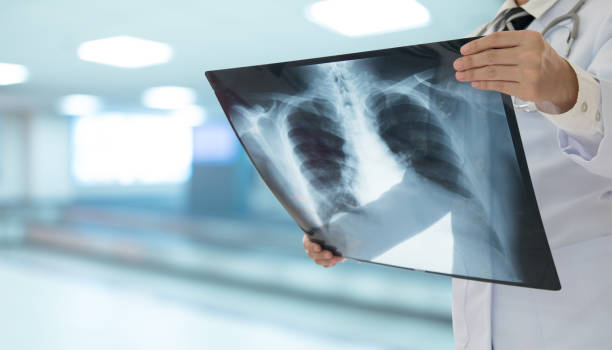
X-ray inspection systems use controlled radiation to capture images of a product’s internal composition, making it possible to identify cracks, voids, contaminants, misalignments, and structural defects that are not visible through conventional visual inspection methods. This capability is especially valuable for manufacturers producing complex or safety-critical components.
As production volumes increase and supply chains become more sophisticated, manual inspection alone is often insufficient to ensure consistent quality. Automated X-ray systems help manufacturers reduce human error while enabling faster and more accurate inspection of high-volume production lines. These solutions also generate digital records that can support traceability and quality audits.
The importance of advanced quality assurance has been highlighted by international organizations promoting stronger industrial standards and safer manufacturing practices. Guidance from the International Organization for Standardization (ISO) underscores the role of robust inspection and quality management systems in improving operational performance and customer confidence.
Key Industries Driving Adoption in China
The electronics sector represents one of the most prominent users of X-ray inspection technology. As semiconductor packaging, printed circuit boards, and miniature electronic assemblies become increasingly complex, manufacturers require precise imaging systems to detect solder joint defects, internal fractures, and assembly inconsistencies. High-resolution X-ray inspection helps maintain product reliability while reducing costly recalls and production waste.
The automotive industry is another major area of adoption. The expansion of electric vehicles, advanced driver assistance systems, and battery technologies has increased the need for non- destructive inspection of critical components. X-ray systems are commonly used to evaluate battery cells, cast metal parts, electronic control units, and welded assemblies, helping manufacturers meet stringent quality expectations.
Food and beverage manufacturers are also integrating X-ray inspection into production lines to improve product safety. These systems can identify foreign materials such as metal fragments, glass, stones, or dense plastic contaminants while simultaneously checking fill levels and packaging
integrity. Regulatory agencies around the world continue to encourage risk-based food safety management approaches that support the use of advanced detection technologies. Information published by the U.S. Food and Drug Administration’s food safety resources reflects the broader industry focus on preventive quality and contamination control.
The Role of Smart Manufacturing and Automation
China’s ongoing investment in smart factories and digital transformation initiatives is creating a favorable environment for the wider deployment of X-ray inspection systems. Manufacturers are increasingly connecting inspection equipment with automated production lines, industrial robotics, and data analytics platforms to create more intelligent quality management processes.
Modern X-ray inspection solutions can be integrated with machine vision software and artificial intelligence algorithms to improve defect recognition. Instead of relying solely on predefined inspection rules, AI-enabled systems can learn from historical inspection data and identify subtle anomalies that may otherwise go unnoticed. This capability helps reduce false rejection rates while improving production consistency.
Another important development is the integration of inspection data into broader industrial Internet of Things (IIoT) ecosystems. Real-time monitoring and centralized analytics enable plant operators to identify trends, predict maintenance requirements, and optimize production workflows. As digital manufacturing becomes more widespread, inspection technologies are expected to play a larger role in data-driven operational decision-making.
Benefits of Non-Destructive Testing Technologies
One of the primary advantages of X-ray inspection systems is their ability to conduct non-destructive testing. Unlike methods that require cutting, dismantling, or otherwise damaging the product being examined, X-ray imaging preserves the integrity of the inspected item. This makes it particularly valuable for expensive, complex, or highly regulated products.
Manufacturers also benefit from reduced material waste and lower production costs because defects can be identified earlier in the manufacturing process. Early detection minimizes the risk of defective products reaching later production stages or entering the market, where recalls and warranty claims can become significantly more expensive.
The technology additionally supports compliance with international quality standards by creating digital inspection records that can be reviewed during audits or customer evaluations. As supply chains become more globally interconnected, the ability to demonstrate consistent quality assurance practices is becoming an important competitive advantage for manufacturers operating in export-oriented industries.
Challenges and Future Industry Developments
Despite the advantages, implementing advanced X-ray inspection systems can involve considerable investment in equipment, installation, and workforce training. Organizations must also ensure that inspection systems comply with radiation safety regulations and that employees receive appropriate operational training. These factors may influence the pace of adoption, particularly among smaller manufacturers.
However, technological innovation continues to improve accessibility and performance. Compact system designs, enhanced imaging resolution, AI-assisted analysis, and faster processing speeds are making X-ray inspection more practical for a broader range of applications. Vendors are also
developing solutions tailored for specialized industries, including pharmaceuticals, aerospace, electronics, and battery manufacturing.
Research institutions and global health and safety organizations continue to emphasize the importance of safe and responsible use of ionizing radiation technologies. Technical guidance from the International Atomic Energy Agency (IAEA) highlights best practices for radiation protection and the secure application of industrial imaging systems.
Outlook for China’s X-Ray Inspection System Industry
The future of X-ray inspection technology in China is closely linked with the country’s broader industrial modernization efforts. As manufacturers pursue greater automation, higher quality benchmarks, and improved product traceability, advanced inspection systems are likely to become an increasingly integral part of production environments.
Demand for reliable non-destructive testing is expected to remain strong across sectors such as electronics, automotive manufacturing, food processing, pharmaceuticals, and precision engineering. The continued evolution of artificial intelligence, machine learning, and connected factory technologies will further expand the capabilities of X-ray inspection platforms, enabling more accurate and efficient quality assurance processes.
For organizations monitoring developments in this segment, the China X-Ray Inspection System report provides additional insights into the factors influencing industry growth, emerging application areas, and the changing landscape of inspection technologies across the country’s manufacturing ecosystem.