
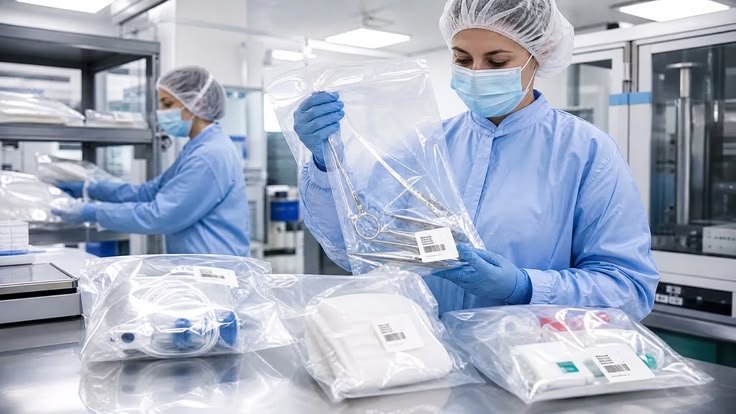

Sterile Packaging: A Guide for Australian Businesses
Medical products often need more than basic wrapping to remain protected during storage, transport, and handling. Surgical instruments, medical devices, diagnostic products, and other healthcare supplies may require packaging designed to support their safety and integrity until they are ready for use. Choosing the right packaging is therefore an important part of product quality and supply chain management.
Sterile packaging is especially important for medical products that must remain sterile until they reach the point of use. The packaging system must be compatible with the product, the intended sterilisation method, and the conditions the package may encounter during distribution. For Australian manufacturers and healthcare suppliers, selecting the right solution can help protect product integrity, reduce avoidable waste, and support consistent packaging processes.
For businesses working within tight budgets, the challenge is finding packaging that meets the necessary requirements without creating unnecessary costs. The cheapest option is not always the best value, particularly if it leads to seal failures, damaged products, or costly rework. A practical approach considers material suitability, equipment performance, quality controls, and long-term operating expenses together.
Why Sterile Packaging Matters in Australia
Australia’s healthcare sector relies on medical products being supplied in appropriate condition and ready for their intended use. Sterile packaging helps protect products that are supplied sterile by supporting the maintenance of sterility until the package is opened, provided that the packaging system and associated processes perform as intended.
A package may travel through several stages before reaching a hospital, clinic, laboratory, or other healthcare facility. During that journey, it can experience handling, compression, vibration, temperature changes, and extended storage. Sterile packaging must be suitable for the product and the expected distribution conditions so that its protective function is maintained.
Packaging failures can have serious commercial consequences. Damaged pouches, compromised seals, or unsuitable materials may result in rejected products, investigations, repackaging, and additional costs. In some circumstances, a package integrity issue may also mean that the product cannot be used as intended.
Reliable sterile packaging helps businesses establish a consistent approach to product protection. When materials, sealing parameters, and inspection procedures are clearly defined, manufacturers can better manage variations and investigate problems. This is particularly valuable for Australian businesses supplying products across large distances or through complex distribution networks.
Understanding Medical Sterile Packaging
Medical sterile packaging is designed for medical products that require a sterile condition until use. It may include pouches, reels, trays, lids, wraps, or specialised containers selected according to the product and the intended sterilisation process.
The packaging must be compatible with the medical device and its sterilisation method. Different processes can impose different requirements on packaging materials, seals, and overall package design. A material suitable for one application may not be suitable for another, so businesses should assess the complete system rather than choosing materials based on appearance or price alone.
Medical sterile packaging must also provide suitable protection during storage and distribution. A lightweight product may need a flexible pouch, while a delicate or heavy instrument may require a more supportive package. Sharp edges, moisture sensitivity, product dimensions, and handling conditions can all influence the packaging design.
Ease of opening is another consideration. Healthcare professionals may need to access sterile products efficiently while following appropriate handling procedures. The package should be designed for its intended use and, where required, support a suitable presentation method.
It is important to understand that packaging alone does not sterilise a product. Sterility depends on the appropriate sterilisation process and suitable controls, while the packaging system must perform its intended protective function. Medical sterile packaging should therefore be developed and evaluated as part of the overall product and quality system.
What Is a Sterile Barrier System?
A sterile barrier system is the packaging component that provides the necessary barrier against microbial contamination and helps maintain the sterile condition of a product until use. It is a central consideration for medical devices supplied in a sterile state.
Sterile packaging and the sterile barrier system must work together with the product, packaging materials, sterilisation method, and distribution process. A package may look intact but still require appropriate testing or inspection to establish whether it meets its performance requirements. Visual appearance alone cannot demonstrate every aspect of package integrity.
Seal quality is one important part of the sterile barrier system. Seals need to meet the relevant specifications and remain intact under the expected storage and distribution conditions. Factors such as material compatibility, sealing temperature, pressure, time, and operator technique can influence the final result.
The packaging design should also consider how the package will be opened. For products requiring sterile presentation, the package may need to allow the user to access the device without unnecessarily compromising the intended handling process.
Australian manufacturers should establish suitable procedures for evaluating and controlling the sterile barrier system. Depending on the product and applicable requirements, this may involve packaging validation, integrity testing, seal assessment, distribution testing, and routine quality checks. The specific activities should be determined by qualified personnel based on the intended application.
Types of Medical Pouch Packaging
Medical pouch packaging is widely used for medical devices and supplies because it can provide a convenient format for packaging, storage, and handling. Pouches are available in different sizes, material structures, and configurations, allowing manufacturers to select an option suited to their products.
Pre-made pouches can simplify packaging operations because they are supplied ready for filling and sealing. They may be appropriate for smaller production runs, specialised devices, or businesses that want a straightforward workflow. However, the pouch material must be compatible with the sealing equipment and the intended sterilisation process.
Roll-stock packaging is another option. It allows certain machines to form packages from reels of material, which can be useful for businesses handling different package lengths or higher production volumes. The equipment and material combination must be selected carefully to support consistent sealing and appropriate package performance.
Medical pouch packaging may use specialised paper-based materials, films, laminates, or combinations designed for particular applications. Different material structures offer different properties, including flexibility, strength, barrier characteristics, and compatibility with sealing methods.
The choice of pouch should reflect the device’s dimensions, weight, shape, sharp edges, and sensitivity to environmental conditions. Businesses should also consider storage, transport, opening requirements, and the relevant quality specifications.
Before committing to a particular medical pouch packaging format, Australian buyers should request technical information and confirm suitability for the intended use. Testing representative samples can help identify compatibility issues before full-scale production begins.
Choosing Sterilization Packaging Materials
Sterilization packaging materials must be selected according to the product, the sterilisation method, and the required packaging performance. Materials that work well in one process may not provide the same performance under different conditions, making careful selection essential.
Flexible materials may include specialised films, laminates, and medical-grade paper-based structures. Rigid trays and protective containers may be appropriate for devices that need additional physical support. The correct choice depends on the packaging design and the protection required throughout the supply chain.
Material compatibility is particularly important when heat sealing is involved. Sterilization packaging materials must work with the selected sealing equipment and process settings. Inappropriate materials or unsuitable sealing conditions can cause weak seals, wrinkles, excessive melting, or other defects that affect package quality.
Businesses should also consider how the material responds to the intended sterilisation process. Relevant properties may include dimensional stability, barrier performance, seal strength, and resistance to handling damage. The manufacturer should provide appropriate technical information to support the selection process.
For price-conscious buyers, comparing material cost alone can be misleading. A lower-priced material may create more waste, require additional handling, or fail to perform adequately in the intended application. A slightly more expensive material may provide better overall value if it supports reliable packaging and reduces preventable defects.
The best approach is to evaluate sterilization packaging materials against documented requirements. Suppliers can provide product information, but the medical device manufacturer remains responsible for determining whether the selected packaging system is suitable for its intended use.
The Role of Sterile Packaging Equipment
Sterile packaging equipment supports the processes used to prepare, form, seal, inspect, and label medical packages. Depending on the operation, equipment may include heat sealers, pouch sealing machines, tray sealing systems, inspection devices, and other packaging machinery.
Heat sealing equipment is commonly used to seal compatible pouches and packaging materials. The equipment must provide appropriate control of the relevant process parameters and support repeatable results. A machine that works well with one material may not be suitable for another, so compatibility should be confirmed before purchasing.
Smaller operations may use manual or semi-automatic equipment for intermittent packaging tasks. Larger manufacturers may require automated systems to handle higher production volumes and reduce repetitive manual work. The right configuration depends on output requirements, available space, operator skills, and the packaging design.
Sterile packaging equipment should also support the quality procedures required by the business. Depending on the application, useful capabilities may include adjustable settings, monitoring features, alarms, process records, and clear operating controls. The value of each feature depends on the actual packaging requirements.
When comparing equipment, Australian businesses should consider more than the purchase price. Maintenance, spare parts, installation, training, technical support, and the expected working life all affect the total investment.
A practical buying process includes reviewing the machine specifications and, where possible, testing representative packaging materials. This helps establish whether the proposed equipment can support the intended application before the business commits to a purchase.
Benefits of Reliable Sterile Packaging
Reliable sterile packaging can help protect medical products from contamination and physical damage when the complete packaging system is properly designed and controlled. For manufacturers and healthcare suppliers, consistent packaging performance supports product quality and dependable distribution.
Another benefit is reduced packaging waste. Defective seals, torn pouches, and unsuitable materials can lead to discarded packages and additional handling. When businesses select appropriate materials and establish consistent procedures, they may reduce preventable defects and improve production efficiency.
Sterile packaging can also support more predictable workflows. Standardised packaging materials, documented settings, and routine quality checks help operators follow the same process across production batches. This can make it easier to identify deviations and investigate problems when they occur.
For businesses supplying healthcare organisations, dependable packaging can strengthen confidence in the product and its presentation. Accurate labelling, suitable package design, and consistent quality checks help support professional handling throughout the supply chain.
However, these benefits depend on proper implementation. Purchasing sterile packaging materials or equipment does not automatically establish that the finished package meets all requirements. Appropriate product-specific evaluation, process controls, and quality assurance remain essential.
Key Factors to Consider When Choosing a Solution
Selecting sterile packaging requires a clear understanding of the product and its intended use. Before comparing materials, equipment, or suppliers, businesses should document the key requirements and use them as a consistent basis for evaluation.
Product characteristics: Consider dimensions, weight, shape, sharp edges, fragility, and sensitivity to moisture or other environmental conditions.
Sterilisation method: Confirm that the packaging materials and design are suitable for the intended process, where sterilisation is required.
Material compatibility: Check that the selected packaging materials work with the sealing equipment and packaging process.
Seal performance: Determine the relevant seal specifications and how the packaging process will be monitored and evaluated.
Distribution conditions: Consider storage duration, transport distance, handling, and the conditions the package may encounter before use.
Production volume: Estimate typical and peak output so the equipment can meet demand without unnecessary expense.
Documentation: Confirm what technical specifications, operating instructions, maintenance information, and quality records are required.
Supplier support: Assess training, spare-parts availability, warranty terms, and technical assistance.
These factors help Australian businesses select sterile packaging based on evidence and practical needs. They also make it easier to compare suppliers fairly and identify potential issues before production begins.
Managing Packaging Costs Without Compromising Quality
Packaging costs can add up quickly, especially for manufacturers producing large volumes of medical devices. However, choosing the lowest-priced materials or equipment may not result in the lowest overall cost. Defects, product damage, downtime, and additional inspections can outweigh the initial savings.
A better approach is to calculate the total cost of the packaging process. Include materials, labour, equipment, maintenance, waste, inspection, storage, and the cost of dealing with defective packages. The relative importance of each factor depends on the business and the product.
Standardising packaging formats where appropriate may help simplify purchasing and inventory management. If several products can use the same validated packaging configuration without compromising their requirements, the business may be able to reduce complexity. Any changes must still be assessed for suitability.
Equipment selection also affects operating costs. A compact machine may be sufficient for a smaller facility, while a higher-volume operation may benefit from automation. Paying for more capacity than the business needs can tie up funds, but selecting a machine that cannot meet demand may create bottlenecks.
Australian buyers should request detailed quotations that clearly identify what is included. Installation, freight, training, maintenance, warranty coverage, and replacement parts can vary between suppliers. Comparing these items alongside machine specifications helps businesses understand the true cost.
The goal is to make sterile packaging reliable and commercially sustainable. Cost savings should come from better planning, appropriate material use, and efficient processes rather than reducing essential product protection.
Australian Regulations and Quality Considerations
Sterile packaging requirements in Australia depend on the medical product, its intended purpose, whether it is supplied sterile, and the regulatory obligations that apply to the manufacturer or sponsor. Businesses should identify the relevant requirements before finalising packaging materials and production procedures.
The Therapeutic Goods Administration regulates medical devices in Australia under the applicable therapeutic goods framework. Depending on the product and business role, relevant obligations may include requirements relating to inclusion in the Australian Register of Therapeutic Goods, conformity assessment, labelling, and other regulatory matters. Businesses should confirm the specific obligations that apply to their circumstances.
For packaging intended for terminally sterilised medical devices, the ISO 11607 series may be relevant. It addresses packaging materials and sterile barrier systems for terminally sterilised medical devices. The applicable parts, editions, and requirements should be confirmed with qualified regulatory or quality personnel.
Conclusion: Choosing the Right Sterile Packaging
Sterile packaging plays an important role in protecting medical products and helping maintain sterility until use when the complete packaging system is properly designed and controlled. For Australian manufacturers and healthcare suppliers, selecting the right materials, equipment, and processes can support product quality and more reliable distribution.